Quality control encompasses the procedures and processes that ensure the production of edible items that meet set specifications and standards. An effective quality Management system comprises raw material testing and inspection, manufacturing process, laboratory analysis, good manufacturing practices, packaging inspection, storage and distribution Management, and product evaluation. The entire process aids in the early identification and elimination of manufacturing defects.
Why Do Food Processing Organizations Need Quality Control Systems?
Edible products may pose health risks to consumers due to the presence of foreign substances such as microorganisms, chemical contaminants, and radioactive substances. On the other hand, poor-quality Management processes can lead to losses incurred due to rejections, contamination, and wastage. An effective Standard Management system can help the food processing industry prevent such losses while also ensuring that the finished products meet the Standard and safety specifications of prospective buyers.
A reliable Standard Management system helps an organization:
- Maintain Standard
- Minimize the risks of contamination
- Reduce wastage and rejected batches of finished products
- Meet customer expectations
- Maintain the shelf life of products
- Ensure compliance with applicable food laws and regulations
- Enhance production efficiency and cost-effectiveness
- Facilitate audits and inspections
- Build the trust and confidence of customers.
New entrants in the processing sector should consider quality Management requirements when designing the processing plant, acquiring machinery, laying out the production process, and putting in place utility systems and procedures.
Key Elements of a Food Quality Management System
Raw Material Inspection
The quality of the raw materials and other supplies used in the manufacturing process largely determines that of the finished products. Therefore, as part of a Standard Management system, edible processors must put in place appropriate procedures for inspecting and testing all supplies against agreed specifications. In addition to appearance and general condition, raw material inspection may involve testing for moisture content, maturity, cleanliness, and temperature.
Good Manufacturing Practices (GMP)
Good manufacturing practices (GMP) are guidelines that provide minimum standards for manufacturing processes and controls. GMP covers a wide range of procedures, including personal hygiene, sanitation, maintenance, pest Management, water Standard, and waste disposal, among others.
All employees must have a good understanding of standard operating procedures and the basic hygiene and safety protocols that apply in the production facility. The entire staff must understand their roles and responsibilities in achieving good manufacturing practices and maintaining a clean working environment.
Process Control
It is important for edible manufacturing organizations to implement appropriate standards and procedures for controlling the production process. Process Management typically entails monitoring process variables such as temperature, pressure, time, moisture content, pH level, and concentration, among others. For instance, an edible processing company that uses thermal processing must monitor and record temperature-time variables at specified points. In most cases, process Management instructions are developed based on the nature of the finished products.
Hazard Analysis and Critical Control Points (HACCP)
Hazard analysis critical control point (HACCP) method is a systematic preventive approach to eatable safety that focuses on the analysis of biological, chemical, and physical hazards associated with production. The method relies on the development of protocols that enable an organization to monitor and supervise potential hazards that may compromise the safety of its products.
A typical HACCP protocol involves:
- Conducting a hazard analysis
- Identifying critical control points (CCP)
- Establishing critical limits for each CCP
- Monitoring CCPs
- Developing corrective measures for deviations
- Verifying that the implemented procedures are effective
- Maintaining appropriate records
By designating critical Supervision points and monitoring them regularly, an organization can develop a proactive approach to identifying and addressing potential deviations in its production process.
Laboratory Testing
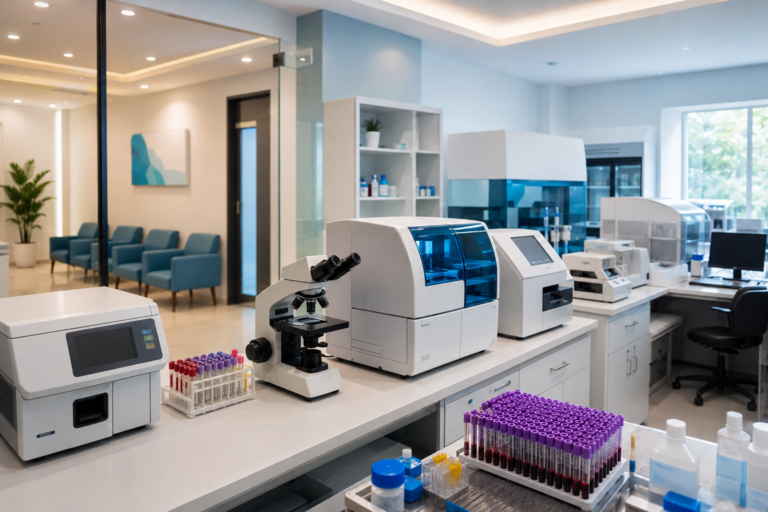
Depending on the nature of the Consumable products, laboratory testing may be necessary to monitor and check various Standard and safety aspects. Common tests performed in food processing organizations include moisture, acidity, pH, and other physical, chemical tests, and microbiological assays such as the detection of E Coli bacteria. The nature of the tests conducted must be determined based on the requirements of the product, regulations, and customer specifications, among other factors.
Packaging Inspections
Packaging performs several functions, ranging from providing information about the contents of the package to protecting the product against contamination and environmental factors such as dampness and physical damage. In addition to a good appearance, Consumables packaging must be of high Standard and free from defects. As part of the quality Supervision system, a Consumables manufacturing organization must conduct regular inspections to ensure that the following aspects of packaging comply with quality standards:
- Seal integrity, bag or wrapper Standard and label
- Printing legibility, pack size coding, and date coding
- Bag material and leak detection tests
- Correct labeling of the contents and batch number
- Date marking procedures and bag material
- Product leak testing and inspection of bag printing for defects
Labeling must also adhere to specified regulations and not be misleading and therefore should be included in the packaging inspection process.
Storage and Distribution Control
Edible products spoilage can occur during the transport and storage of finished products. Therefore, a Consumables processing organization must ensure that transportation and storage procedures and equipment are fit for use and appropriate for the class of goods being handled. In addition, it is important to monitor environmental conditions such as temperature and humidity and ensure that the storage area is clean and free from pests. Maintaining good stock rotation practices also helps to ensure that expired or faulty goods are not dispatched to customers.
Documentation and Record Keeping
A well-documented Standard Supervision system enables an organization to demonstrate the effectiveness of its management system in meeting quality standards and specifications. For instance, records provide documentary evidence that raw materials have been inspected and tested and that the results conformed to set standards. Similarly, record-keeping enables an organization to trace the cause of quality defects in case of a product complaint.
Some of the key records that must be maintained in a manufacturing organization include:
- Raw material inspection records
- Supplier qualification records
- Production batch records
- Cleaning records
- Maintenance records
- Laboratory test results and records
- Temperature records
- Packaging inspection records
- Corrective action records
- Employee training records
- Records of approved finished products
Employee Training
Without adequate training, even the most advanced Consumable processing equipment will not be able to produce high-quality products. Employees must have a solid understanding of the basic hygiene and safety rules that underpin the manufacturing process. In addition, they must know how to operate assigned equipment and carry out routine maintenance. They should also understand how to perform various quality control measures, address quality defects, and maintain good documentation records.
Employees should receive refresher training on such topics as good manufacturing practices, personal hygiene, and standard operating procedures.
Quality Control Equipment
The nature of equipment needed for Standard control will vary depending on the products and processes used in a food processing organization. Some of the common equipment used in Standard control in the food processing industry include weighing equipment, moisture, and pH meters, thermometers, laboratory analyzing equipment such as spectrometers, metal detectors, bag sealing inspection machines, storage equipment, and others applicable to the product being manufactured.
It is important to conduct regular calibration and servicing of all equipment to ensure that they are operating at optimal levels and are delivering accurate results.
Corrective and Preventive Actions
In most cases, simply rejecting a batch of rejected products is not sufficient, and therefore a corrective action system should be implemented. A corrective action system typically has well-defined procedures for addressing quality-related incidents and deviations in the manufacturing process. It also provides guidelines for carrying out root cause analysis and implementing corrective and preventive measures.
Corrective actions usually follow a six-step approach, namely:
- Recognizing a deviation
- Isolating the affected material
- Conducting a detailed investigation to identify the cause of the deviation
- Taking corrective action
- Verifying the effectiveness of the corrective action
- Documenting the findings and lessons learned
Once a quality deviation has occurred, the corrective action team must address the following questions:
- What went wrong?
- What caused the deviation?
- How can the problem be prevented in the future?
By taking corrective and preventive actions, an organization can minimize the likelihood of similar incidents from occurring.
How To Design a Quality Control System for New Food Processing Organizations
New entrants in the Edible products processing sector must incorporate quality Supervision measures in every step of the way. While planning a Consumables processing plant, entrepreneurs must consider a wide range of factors, including the most appropriate methods for laying out the layout, ensuring proper drainage, ventilating the building, and dealing with waste.
A practical approach is to define product specifications and address the associated inspection requirements before developing the process steps for manufacturing the Consumable items. This way, a reliable Standard Supervision system can be designed with clearly defined testing procedures and documentation requirements.
Adequate employee training, as well as the implementation of good hygiene and manufacturing practices, is also vital in ensuring that the production process runs smoothly without defects.
Conclusion
A robust quality control system is vital in the operations of every food processing organization, and therefore new entrants must invest effort and resources to ensure that it is operational from day one. An effective system will comprise a combination of various elements, including inspection and testing of raw materials, good manufacturing practices, process control, HACCP, laboratory tests, proper packaging, staff training, and documentation. For new entrants in the Consumables processing sector, developing a quality Supervision system is essential because it minimizes wastage, facilitates adherence to applicable regulations, and boosts consumer confidence in the brand.
FAQs
Why is quality control important in food processing?
It ensures that Edible products are safe for human consumption and minimizes wastage, rejection of products, and customer complaints.
What are the key elements of a food quality control system?
The main elements of a Edible products quality Supervision system include raw material inspection, good manufacturing practices, process control, HACCP, laboratory testing, packaging inspection, storage control, employee training, and documentation.
What does HACCP means in the food industry?
HACCP stands for Hazard Analysis and Critical Control Point. It is a preventive food safety management system that focuses on the analysis of biological, chemical, and physical hazards in food production.
Is laboratory testing mandatory in a food processing organization?
Not necessarily. The need and nature of laboratory testing will depend on the type of product being produced, the process used, the applicable regulations, and the requirements of prospective buyers.
How can food manufacturing organizations minimize contamination?
Food processing organizations can minimize contamination by using hygienic equipment and machinery, adhering to good manufacturing practices, and employing appropriate process control measures.
Why is documentation important in the food manufacturing industry?
Documentation provides evidence that the production process is under control and that all specifications and requirements are being met.
What factors should entrepreneurs consider when planning to establish a food processing organization?
When planning to start a food processing organization, entrepreneurs should consider such issues as the nature of raw materials, production process, machinery, layout, utility systems, hygienic practices, quality control and testing procedures, packaging, storage, regulations, manpower and training, and waste disposal.
How often should employees be trained in food manufacturing organizations?
Besides orientation training, employees should receive recurrent training on such issues as good manufacturing practices, personal hygiene, standard operating procedures, and equipment operation and maintenance.